Design & Craftsmanship
Integrating RFID-Blocking Technology in Leather Wallets: A Manufacturer’s Perspective on Balancing Craftsmanship and Functionality
Published on Nov 1, 2026
Executive Summary for B2B Sourcing When brands source RFID-blocking leather goods, the challenge rarely lies in the material itself, but in the manufacturing execution. Based on our production line data, the optimal balance between tactile feel and signal attenuation is achieved using a 0.08mm–0.10mm Copper/Nickel (Cu/Ni) conductive fabric. Combining this with an 8-9 SPI (Stitches Per Inch) sewing standard and a turned-edge construction effectively mitigates "pinhole signal leakage." Furthermore, implementing a 100% in-line inspection for the 13.56 MHz frequency is the most reliable way for procurement teams to ensure batch consistency and minimize end-consumer return rates (RMAs).
I. Deconstructing Amazon Negative Reviews: Why Do Consumer RFID Wallets "Fail"?
As a manufacturing partner for overseas SLG (Small Leather Goods) brands, our team regularly reviews end-market feedback alongside our clients. Analyzing 1-star reviews for RFID wallets on e-commerce platforms reveals two major technical blind spots:
1. "It doesn't block my office key card or hotel room key."
- The Manufacturing Reality (Frequency Discrepancy): This is a common physics mismatch. Most legacy access cards and hotel keys operate on a low frequency (125 kHz), whereas modern credit cards, passports, and NFC-enabled cards operate on a high frequency (13.56 MHz). Standard RFID wallets are engineered specifically to protect high-frequency financial assets. Shielding against 125 kHz requires significantly thicker absorbing materials, which adds unacceptable bulk to minimalist designs and compromises the premium feel of the leather. We always advise our B2B clients to explicitly state this frequency distinction in their product listings to manage consumer expectations and reduce unjustified returns.
2. "The outer card slots still got scanned."
- The Manufacturing Reality (Pinhole Signal Leakage): This defect usually originates on the sewing floor. If the needle holes are too large or the stitching is too dense, it compromises the physical structure of the "Faraday cage." Without proper edge-wrapping, strong scanner signals can penetrate these micro-gaps via an antenna effect, leading to leakage on the outermost cards. This is a direct reflection of a factory's precision management and QC protocols.
II. Sourcing the Shielding Lining: The Trade-off Between Thickness, Security, and Hand-Feel
In minimalist wallet designs, space is at an absolute premium. Having tested nearly all available shielding materials in our R&D room, we've found that material selection is a process of strategic trade-offs:
- Aluminum/Tin Foil Coatings
- Production Feedback: Cost-effective with baseline shielding. However, it tends to produce a cheap "crinkling" sound when handled. More critically, repeated folding causes metal fatigue and cracking along the creases. We strongly advise against this material for premium vegetable-tanned leather projects.
- Carbon Fiber Shielding
- Production Feedback: Highly durable with excellent blocking capabilities, ideal for hard-shell cardholders. However, its rigidity makes it un-stitchable and incompatible with the natural drape and flexibility of soft leather.
- Cu/Ni Conductive Fabric (Copper/Nickel)
- Production Feedback: This is our standard specification for bulk orders and the industry benchmark. It features a polyester grid plated with copper and nickel—yielding a silk-like softness and highly stable electromagnetic attenuation (>60dB).
- Thickness Pitfalls: Even with the right material, thickness dictates the final quality. We strictly spec our fabric between 0.08mm and 0.10mm. Below 0.08mm, it is prone to tearing during the gluing or leather skiving processes. Above 0.15mm, a standard bifold wallet with 6 card slots will gain nearly 1mm in edge thickness, severely degrading the wallet's slim profile and edge-paint aesthetics.
III. From Prototype to Mass Production: Eliminating "Pinhole Leakage" on the Assembly Line
Premium materials require premium craftsmanship. To prevent signal leakage and ensure lot-to-lot consistency, we focus on three critical production stages:
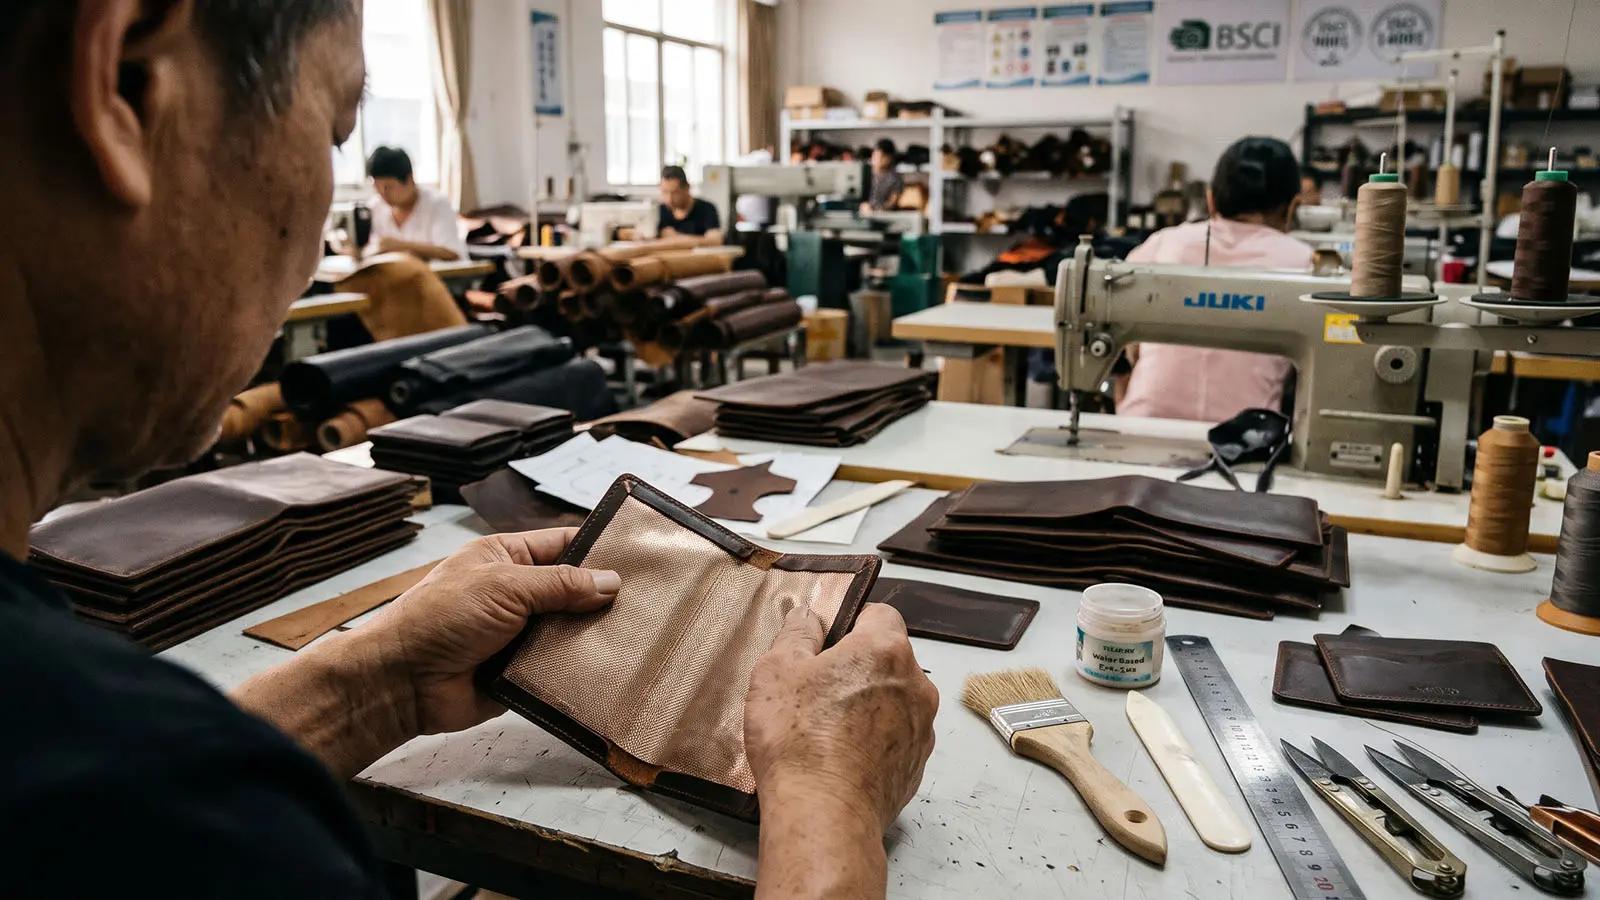
1. Full-Wrap Turned-Edge Construction A common cost-cutting method is raw-edge construction, where leather, lining, and RFID fabric are cut flush and stitched, leaving the edges vulnerable to signal penetration. Our standard operating procedure (SOP) requires the die-cut RFID fabric to be 1.5mm smaller than the leather piece. After applying water-based eco-glue, we utilize a turned-edge technique to fully encapsulate the conductive fabric within the leather. This prevents edge leakage and ensures the subsequent edge paint (edge burnishing) adheres perfectly to the leather, preventing peeling and splitting over time.
2. Calibrating Stitches Per Inch (SPI) Every needle puncture is a hurdle for physical shielding. While some brands prefer a rugged, wide stitch and others a refined, dense French stitch, our baseline for RFID-lined slots is 8 to 9 SPI. If the stitching is too dense, the continuous perforations enlarge the insulation gaps, degrading the shielding rate. Our operators also utilize round-point sewing needles (rather than sharp diamond awls) to gently push the conductive metal threads aside rather than severing them.
3. Lamination Flatness Control If the RFID fabric wrinkles during lamination, it not only ruins the surface aesthetics of the leather but also creates uneven stress points that accelerate wear and tear as end-users continuously insert and remove cards. We utilize roller gluing machines combined with cold-press equipment to ensure the conductive fabric and leather bond seamlessly and remain perfectly flat.
IV. Quality Control for Bulk Orders: Replacing Guesswork with Protocol
For B2B buyers, consistency across bulk runs is more critical than a perfect golden sample. To minimize RMA rates, we have implemented a structured QC pipeline on our factory floor:
- Incoming Quality Control (IQC): Every new batch of Cu/Ni fabric is scanned in our lab using a Vector Network Analyzer (VNA) to confirm electromagnetic attenuation meets the >60dB threshold in the target frequency bands before entering the production floor.
- In-Line Sub-Assembly Inspection: Before the wallet is fully assembled, QC inspectors perform rapid blind sweeps on the stitched card slots using industrial 13.56 MHz RFID testers to catch any structural anomalies early.
- Finished Goods AQL Testing: Prior to final packaging, we conduct inspections based on AQL 1.5 standards. We insert test cards into the slots and use high-powered scanners from the front, back, and edges (a 360-degree sweep) to simulate real-world usage. Only units that trigger zero signal response are cleared for shipping.
FAQ: Common Technical Questions from Procurement Teams
Q1: Do your wallets block all scanning devices?
Frankly, no single wallet can block all frequencies without compromising design. Our products are engineered specifically to shield the 13.56 MHz band (credit cards, passports, IC cards). To maintain the slim profile of the leather, we do not incorporate the thick absorbing materials required for 125 kHz legacy access cards. We highly recommend clarifying this in your e-commerce listings to prevent unjustified negative reviews; consumers are generally very understanding when the physics trade-off is explained.
Q2: Will water exposure or rain damage the RFID shielding?
The Cu/Ni fabric itself is highly oxidation-resistant, so brief splashes will not degrade its shielding capabilities if dried promptly. However, as vegetable-tanned leather is naturally sensitive to moisture, prolonged water exposure will damage the leather's fibers and natural oils. We advise including standard leather-care warnings for the end-consumer.
Q3: I want to source an ultra-minimalist cardholder. Will the RFID layer make it too bulky?
This is where our manufacturing capabilities shine. By utilizing 0.08mm Cu/Ni fabric and precision leather skiving (thinning the leather edges down to 0.6mm), we eliminate the bulk. The tactile difference between our RFID and non-RFID minimalist wallets is virtually imperceptible to the touch, fully satisfying minimalist design requirements.
Q4: Can we design a "Tap-and-Go" wallet where one specific outer slot is left unshielded for transit cards?
Absolutely. We frequently manufacture these commuter-friendly designs for brand clients. During the die-cutting and sewing phases, we selectively hollow out or bypass the shielding layer for the designated outer slot. This keeps the main compartment secure while allowing contactless transit scans without removing the card. This requires high-precision tooling and alignment, which is a mature, standardized process on our assembly line.